
How Are Rolling Mill Rolls Ground?
Grinding of rolling mill rolls is carried out for the purpose of roll maintenance and repair. This process has a direct impact on optimal performance and service life of the rolls and is performed to eliminate defects and damage. By removing a small amount of material from the surface, roll grinding helps restore the original shape and geometry of the roll.
In this article from the Mazs Group magazine, we examine the types of rolling roll grinding, the components of the grinding process, and how it is performed. Finally, we outline important points that must be observed during grinding operations.
This article examines the following topics:
Types of Rolling Roll Grinding
In both hot strip rolling lines and cold strip rolling lines, rolls play a critical role in shaping steel sheets. Therefore, regular inspection and maintenance of rolls are essential, and any damage must be repaired when necessary. For example, since cold-rolled sheets require high surface quality, any defect on the roll surface is transferred to the cold-rolled product.
One method used to eliminate surface defects of rolling mill rolls is grinding. Grinding has various types, each used for a specific purpose. Grinding machines include cylindrical grinding with centers, centerless cylindrical grinding, internal grinding, and surface grinding.
Depending on the size, shape, and fixturing of the workpiece, different grinding processes are applied. Common methods for grinding rolling mill rolls include centerless grinding and cylindrical grinding with centers.
High-precision reversing cold rolling mill engineered for uniform thickness, superior surface quality, and reliable long-term performance.
Components of the Grinding Process
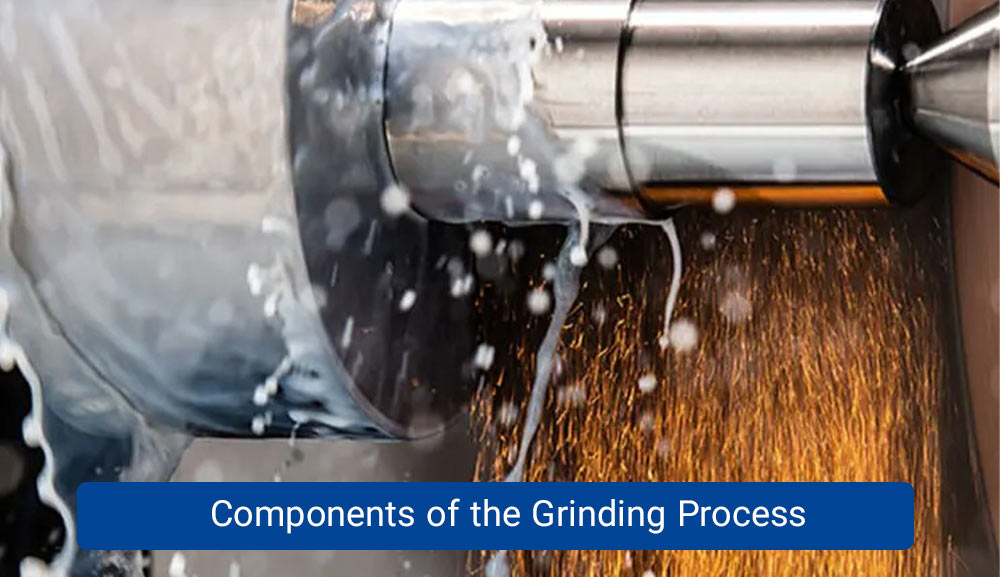
The most important component of the grinding process is the grinding wheel. The grinding wheel removes material from the surface. It is made of abrasive grains bonded together with a very strong bonding material. These abrasive materials have very high hardness and strength. For grinding rolling mill rolls, abrasives such as aluminum oxide or cubic boron nitride (CBN) can be used. Silicon carbide abrasives may also be used, but they are not very suitable for grinding steel components.
The abrasive grain size is selected based on the required surface finish. A grinding machine consists of a drive motor and a machine bed. The motor rotates the grinding wheel at the desired speed, while the bed holds the workpiece in a fixture. Another essential component of the grinding process is the coolant system, which is used to prevent excessive temperature rise in the workpiece during operation.
The grinding result largely depends on the stress between the wheel and the roll at the contact point. Stress in the grinding zone depends on several factors, including wheel speed, roll speed, cross-feed or traverse rate, infeed rate, and the type and flow rate of the coolant.
How Is Rolling Roll Grinding Performed?
At the beginning of the grinding operation, the roll is transferred to the grinding machine using an overhead crane and placed on fixed supports. The purpose of roll grinding is to remove surface defects, improve quality, and create the desired crown on the roll surface. The crown refers to the curvature present on rolls used in hot and cold rolling lines and must be carefully checked.
The grinding process consists of three stages:
- Rough grinding: For primary material removal and crown formation.
- Semi-finishing: To adjust and refine the crown created during rough grinding.
- Finishing: To polish the surface and prepare it for the tandem rolling line.
Below, the grinding operations for rolling mill rolls using cylindrical grinding with centers and centerless grinding methods are explained.
In cylindrical grinding with centers, the external cylindrical surface and shoulders of the roll are ground. In this method, the workpiece is positioned between centers or mounted on a chuck. Motors rotate the roll and the grinding wheel at different speeds.
Since rolls in strip rolling lines are large and heavy, the table and workpiece remain stationary while the grinding wheel performs a reciprocating motion. Roll grinding machines can grind rolls with diameters of up to 1.8 meters. For this reason, cylindrical grinding with centers is also referred to as axial grinding, as the workpiece is mounted on a vertical or horizontal axis.
In centerless grinding of rolling mill rolls, the workpiece is supported by a support blade. In this type of grinding, the roll does not need to be clamped between centers or other fixtures, and no axial drive is required to rotate the workpiece. The roll is positioned between the grinding wheel and the regulating wheel, which presses it against the grinding wheel.
Both the grinding wheel and the regulating wheel rotate clockwise, while the roll rotates counterclockwise. During this process, the support blade underneath the roll provides support. Since force is not applied to the ends of the workpiece in this method, it is particularly suitable for grinding long rolls.
Points to Be Observed During Grinding
During rolling roll grinding, several important points must be considered, including:
- Rolls must be positioned accurately on the machine.
- To prevent bending during grinding, the workpiece must be securely clamped using magnetic tables, chucks, or fixtures.
- To avoid vibration—especially when high dimensional accuracy is required—discontinuous surfaces should be avoided.
- Before grinding, the roll neck should be smoothed using abrasive tools.
- Throughout all grinding stages, the roll diameter must be measured frequently and accurately, and crown deviations must be corrected during rough grinding.
- The concentration of the coolant must be maintained within a standard range at all times.
- The grinding wheel material must be selected so that it is neither too soft nor too hard.
Conclusion
In this article from Mazs Group, we discussed the grinding of rolling mill rolls. We explained that hot and cold rolling rolls require regular inspection and repair to prevent defects from being transferred to steel sheets. One effective method for eliminating surface damage on rolls is grinding.
As discussed, this process significantly contributes to optimal roll performance and increased service life. This article reviewed the types of rolling roll grinding, the components of the grinding process, and the operational procedures involved. Finally, key considerations that must be observed during roll grinding were presented.
FAQ
Grinding is necessary to remove surface defects, restore the original geometry of the roll, and ensure proper crown formation. This process improves product quality, enhances rolling performance, and extends the service life of the rolls.
The grinding frequency depends on operating conditions such as rolling load, material type, surface wear, and production volume. Typically, rolls are ground after a certain number of rolling cycles or when surface defects and dimensional deviations are detected.
The most common methods are cylindrical grinding with centers and centerless grinding. Other methods such as internal grinding and surface grinding may also be used depending on roll design and application.
Common abrasives include aluminum oxide and cubic boron nitride (CBN). Silicon carbide can also be used, but it is generally not recommended for grinding steel rolls due to lower performance.


