
Everything About Eddy Current Testing (ECT)
In industries, in order to ensure the quality of conductive components and to examine them for defects such as cracks, corrosion, or other issues, inspections are necessary. Eddy Current Testing is among the non-destructive, fast, and accurate methods used for testing components as well as for weld inspection. The principle of this test is electromagnetic induction. During the inspection of the component under test, any change in the eddy current pattern indicates that there is a problem in the component. In this article, we will discuss ECT in detail, including its applications, testing method, weld inspection by eddy current testing, and the advantages and disadvantages of this method. For more information about this test, continue with this article from Mazs Group Magazine.
This article examines the following topics:
What is Eddy Current Testing?
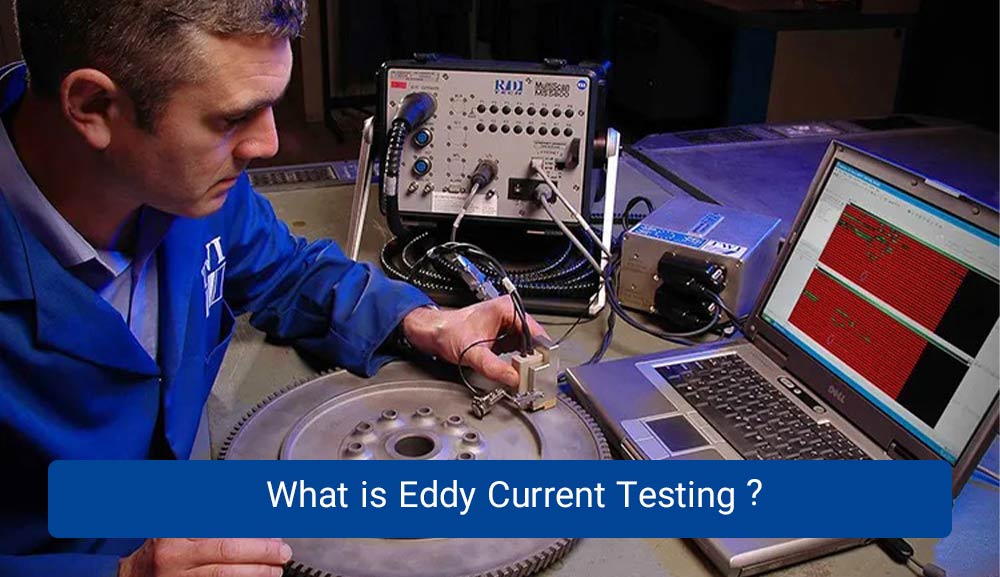
Eddy current testing is a non-destructive test used for component examination and weld inspection. With eddy current testing, defects in electrically conductive materials can be detected. Another name for it is Eddy Current Testing (ECT). The eddy current device generates a magnetic current and detects defects such as cracks, corrosion, bubbles, and thickness variations due to corrosion, which may occur on pipes produced in pipeline and profile production lines.
To fully understand what eddy currents are, we need to know the law of electromagnetic induction. This law states that when a conductive object moves in an external field, it causes a change in magnetic flux, producing an electromotive force. This force enters the circuit and creates scattered currents opposite to the changes of the original magnetic field. These currents are called eddy currents.
Although eddy currents are useful and applied in industry—one of their uses being non-destructive testing—they also have a destructive effect. This destructive effect is power loss in transformers due to heat generation. In this test, six types of probes are used that can detect defects in different directions. These probes include the pancake probe, theta probe, ordinary uniform probe, uniform probe with special coil, pulse-point probe, and TR probe. Each of these probes has its own characteristics and applications.
Mazs Group provides advanced Cut to Length Line machines designed for precision sheet metal processing. Our solutions ensure high accuracy, efficiency, and durability for various industrial applications. Explore our Cut to Length Line category to find the right system for your production needs.
Principle of Eddy Current Testing
The principle of eddy current testing is electromagnetic induction. This test interferes with the magnetic field produced by the device. When the component has a defect, the current applied to it changes. The pipe testing device detects surface defects of pipes using magnetic particles. This test is used to detect surface defects in materials such as copper, aluminum, stainless steel, carbon steel, brass, and titanium.
Applications of Eddy Current Testing
Now let’s see what the applications of eddy current testing are. ECT detects discontinuities on the surface or near-surface of conductive components. Using this test, the maximum area of the component can be inspected in the shortest time. Applications of eddy current testing include thickness measurement, corrosion assessment, evaluation of heat treatment quality, determination of material type and microstructure, material sorting, and detection of discontinuities in components.
Industrial applications include weld inspection, inspection of surface defects in products such as pipes and profiles, rods and cast billets, roller inspection, corrosion assessment of structures, ship hulls and tanks, evaluation of steel strength and hardness, condenser tube inspection, pipe and wiring testing, electromagnetic brakes and stoves, electromagnetic propulsion trains, and NDT testing.
Eddy Current Testing Method
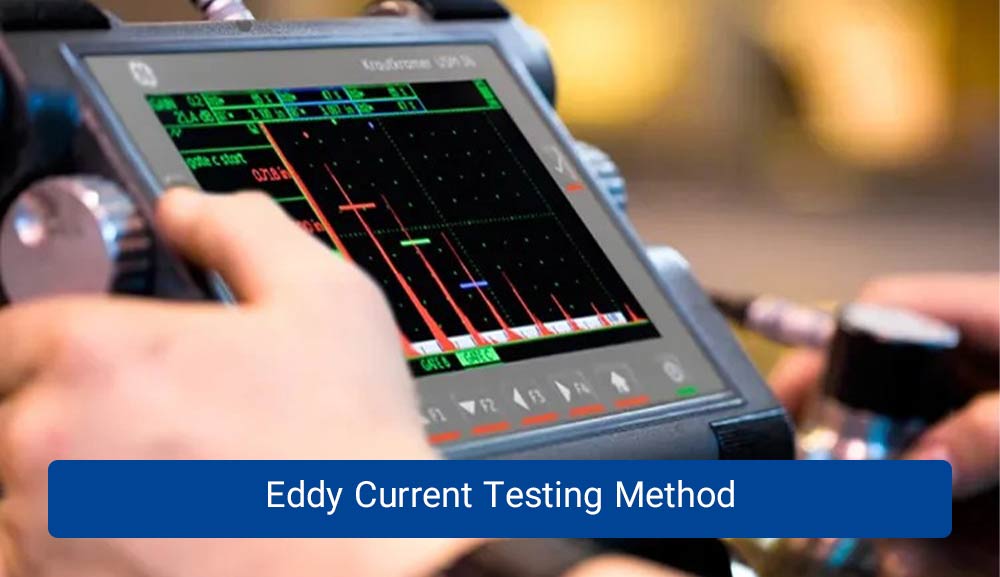
As mentioned, eddy current testing is one of the inspection methods for pipes based on electromagnetic induction. An alternating current flows through the coil or probe of the device, producing a magnetic field. When the probe is brought close to an electrically conductive component, eddy currents flow through the metal, generating a magnetic field. Since ECT is a comparative method, first a sound component is considered as a reference sample, and the test is performed on it, with the results recorded. Then the target component is tested, and the results are compared with those of the sound sample.
Changes in the results indicate the presence of problems such as discontinuities like cracks in the tested component. If discontinuities exist in the component, changes in the eddy current pattern can be observed. Using this method, pipes used in industries can be inspected. A hydrostatic testing device is also used for testing pressure pipes, showing the durability of the pipe under pressure.
Weld Inspection Using Eddy Current Testing (ECT)
As mentioned, weld inspection is one of the industrial applications of eddy current testing. Welding is used in many industries, including gas, oil, petrochemicals, construction, automotive, aerospace, and more. Welding is highly sensitive, and if defects that occur are not detected and corrected, they can cause problems and damages, leading to sudden failures.
Therefore, weld inspection is essential for increasing productivity. The occurrence of cracks or tears in the weld zone is among the problems of pipe, tube, and weld seam production. These can be inspected by using eddy current testing, which is a non-destructive testing method. The advantages of this test have made it one of the main methods for weld inspection.
Observing Changes in Eddy Currents
When eddy current testing is used to detect defects in a component, if discontinuities exist, changes in the eddy current pattern can be observed. For example, if there is a crack, bubble, or cavity in the tested component, the eddy current pattern decreases or changes. The same applies to changes in the chemical composition of the material. This can change electrical resistance, and ultimately, the eddy current pattern. By applying eddy current testing to steel pipes, the likelihood of cracks and the need for steel pipe leak repair can be reduced.
Advantages and Disadvantages of Eddy Current Testing
The use of eddy current testing has several advantages. For inspecting pipes produced in seamless pipe production lines, an offline eddy current device is used. Eddy current testing is a non-destructive test, meaning it does not damage the component. It is a fast test that allows large areas of a component to be examined in a short time. This test is very suitable for determining the material type. Another advantage is that no couplant is needed to connect the component to the probe.
However, ECT also has disadvantages. One limitation is that only conductive components can be inspected. Eddy current testing is a comparative method and requires a sound sample. Also, this test can only detect surface defects, with limited penetration depth. To inspect deeper areas of components, ultrasonic testing can be used.
Conclusion
In this article from Mazs Group Magazine, we presented useful information about eddy current testing. We explained what ECT is and mentioned that this test is based on electromagnetic current and can detect surface defects in conductive components in the shortest possible time. Since welding plays an important role in various industries, it must be inspected with this test to prevent potential failures. The use of this test is not limited to weld inspection; it is also applied for detecting surface defects in pipes and profiles, assessing steel hardness, and many other cases discussed in this article. In addition, we presented the advantages and disadvantages of this test.
FAQ
ECT can identify cracks, corrosion, pitting, porosity, thickness variations, and other discontinuities on or near the surface of conductive components.
ECT is suitable for conductive materials such as aluminum, copper, stainless steel, carbon steel, brass, and titanium.
Yes, ECT is one of the most effective methods for non-destructive weld inspection. It helps identify cracks, porosity, and other discontinuities in weld seams, preventing costly failures in industries like oil & gas, construction, and aerospace.
Advantages:
Non-destructive and fast inspection method
Detects surface and near-surface defects accurately
No need for direct contact or couplant
Disadvantages:
Limited penetration depth
Suitable only for conductive materials
Results can be affected by material properties and geometry
Eddy current testing is used on conductive materials such as metals to detect surface and near-surface defects, measure thickness, and verify material properties in tubes, pipes, sheets, and welded joints.


